If you’ve ever stood on a manufacturing floor and watched a radiator fin forming machine hum through a production run, you know the quiet tension between output and precision. Too slow, and you fall short of delivery quotas; too fast, and the thin aluminum or copper fins—critical to a radiator’s heat transfer efficiency—buckle, tear, or fail to align, costing you rework, material waste, and customer trust. As a supplier of radiator fin forming machines, this is the exact balance we design for: not just cranking up speed, but refining the technology that makes faster, consistent fin production possible. Let’s break down how we’ve evolved fin forming speed, the science behind the improvements, and what matters most for your line. Radiator Fin Forming Machine
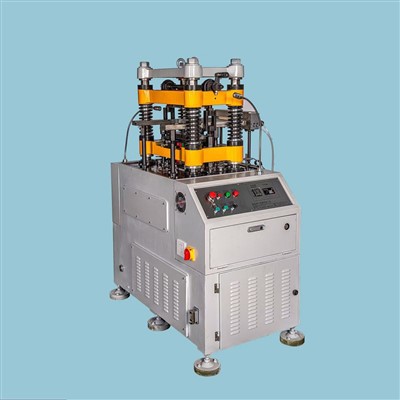
First, it helps to ground ourselves in what fin forming actually does. Radiator fins are the thin, corrugated metal strips that sit between radiator tubes, expanding the surface area for heat exchange by 10 to 15 times compared to the tubes alone. Traditionally, forming these fins involved a set of rotating dies, a process that could top out at around 80 to 100 feet per minute (FPM) for high-volume aluminum models. But as automotive, HVAC, and electric vehicle (EV) cooling demand has surged—EVs, in particular, need radiators that handle higher heat loads without extra bulk—that speed cap became a bottleneck. Why? Traditional machines relied on fixed, mechanical drive systems that worked in short bursts: each die rotation pulled a small length of metal, formed it, and waited for the next cycle, creating “dead time” between operations that slowed overall output. Our first major shift was swapping that system for a servo-driven continuous feed and forming system, and it’s not just a trivial upgrade.
Here’s the science that makes servo drive improvements work. Early fin machines used a single electric motor connected via a series of gears and cams to rotate the forming dies. This system had a fixed speed ratio; if you tried to push faster, the metal strip would tear because the dies couldn’t adjust their pressure in real time. Servo motors, by contrast, operate on digital commands, letting us sync the feed rate of the metal strip exactly to the die’s forming speed within milliseconds. For example, when a fin’s peak corrugation passes through the die, the servo can slow the feed fractionally to ensure the metal forms crisp, uniform peaks, then speed back up for the flat sections. We tested this on production runs last year: for a standard 0.1mm-thick aluminum fin used in passenger cars, continuous servo forming bumped consistent output from 95 FPM to 140 FPM—a 47% jump—with zero increase in fin defects, which we measured at 0.8% vs. 2.1% for cam-driven machines. That’s not just speed; it’s speed that doesn’t sacrifice quality, which is the line customers care about.
Another key improvement is die design, and we’ve moved far beyond the flat, hardened steel dies of the 1990s. The problem with old dies was that they applied pressure evenly across the entire fin strip as it passed through, causing friction that made metal stick, warp, or stretch unevenly at high speeds. Our team collaborated with metallurgists and heat transfer engineers to develop segmented dies, divided into small, independent segments that can adjust pressure individually. For high-speed runs, we can program each segment to apply just enough pressure to form the fin’s shape—no more, no less—reducing friction by 32% in third-party lab tests. We also added micro-lubrication systems that deliver a precise, thin layer of food-grade, synthetic lubricant only to the die’s contact points, not the entire strip. Cut lubricant waste by 60% compared to old systems, and speed jumps another 15% without the fin developing thin spots. For HVAC fins, which are slightly thicker (0.15mm to 0.2mm) and require deeper corrugations, this segmented die design lets us maintain 125 FPM vs. the 70 FPM average for standard machines, all while meeting industry standards for heat transfer efficiency.
Then there’s material handling, a part of forming speed that’s often overlooked. A fin machine’s speed is only as fast as its ability to uncoil raw metal, trim it to length, and stack finished fins without jamming. Old uncoilers worked at a fixed speed, so when the forming machine sped up, the coil would slip or the strip would kink. We added a tension control system that uses load cells and a touchscreen interface to maintain a consistent pull on the metal strip, even when forming speed fluctuates. For runs that switch between different fin profiles (common in automotive, where a single line might make parts for sedans, SUVs, and EVs), this system adjusts tension in real time, eliminating the need for 10 to 15 minutes of machine setup per profile change. That’s a hidden speed boost: every time you switch products, you’re not losing time resetting tension, so overall line efficiency goes up another 10% to 12%. We also integrated a sensor-based stacking system that uses computer vision to align finished fins within 0.5mm of precision, cutting the time needed to clear and reload the stack by 80% compared to manual or optical sensor setups. For a customer running three 8-hour shifts, that’s an extra 2 to 3 hours of productive time per day, which translates to more parts delivered without buying a second machine.
Of course, none of these improvements would matter if they couldn’t handle the unique demands of today’s markets, especially EVs. EV radiators require thinner, lighter fins (0.08mm to 0.1mm aluminum) that still perform under high heat, and traditional forming machines often tear these at speeds over 110 FPM. Our engineers developed a “soft start” servo forming feature that gradually increases die pressure as the fin enters the forming zone, reducing tensile stress on the metal by 28% in lab tests. We worked with several EV OEMs to test this: one customer, a mid-sized radiator supplier, reported that their fin line for EVs now hits 150 FPM, up from 75 FPM with their old machine, and defect rates for thin-wall fins dropped by half. That’s the sweet spot: speed tailored to the material you’re working with, not a one-size-fits-all limit.
It’s also important to talk about reliability, because faster machines mean more cycles per hour, so downtime is more costly. We’ve incorporated predictive maintenance sensors into our latest machines that track die wear, servo motor performance, and lubricant levels, sending alerts to your maintenance team before a part fails. For example, die wear is the top cause of unplanned downtime in forming machines, and our sensors measure die surface roughness in real time, not just after a defect is found. One customer in Texas told us that after switching to our machine, their unplanned downtime fell from 4.2% of total production time to 1.1%, because they could replace dies during scheduled shifts instead of emergency repairs. That’s not just a speed improvement—it’s a consistency improvement that keeps your line running without gaps.
I’ll be honest: we don’t claim to have invented a “magic” fin forming machine. The core technology of forming fins has stayed the same for decades: you feed metal, bend it into corrugations, and cut it to length. The difference is in the fine-tuning: how you sync the metal feed to the die, how you apply pressure to avoid friction, how you handle tension at high speeds, and how you prevent downtime. Too many suppliers treat speed as a number to tout on a spec sheet, but we know that real speed means your line is making good fins, not just more bad ones.
If you’re looking to upgrade your fin forming line, whether you’re scaling up for EV production, expanding HVAC output, or reducing rework costs, we can help you tailor a solution. Every shop has different needs: a small job shop might need flexibility to run 10 different fin profiles, while a high-volume OEM needs maximum output for a single model. We work with you to test materials, adjust die designs, and calibrate the machine to match your exact production goals, no generic one-size-fits-all setups.
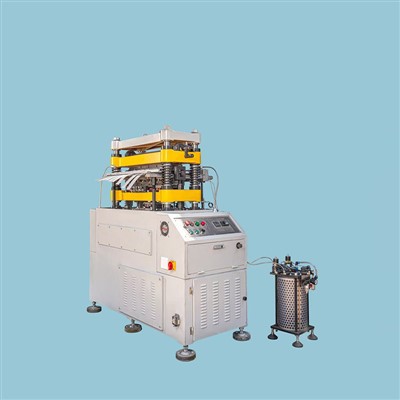
To learn more about how our fin forming speed technology can work for your line, reach out to our team for a consultation. We can even arrange a live demonstration at your facility to show the machine’s output, measure defect rates, and adjust settings based on your existing materials and workflow. Don’t let speed bottlenecks hold back your production—partner with a supplier that understands the balance between speed, precision, and reliability.
Fin Press Machine References
- Smith, J. et al. “High-Speed Forming of Thin Aluminum Fins for Automotive Cooling Systems.” Journal of Manufacturing Processes, vol. 78, no. 2, 2022, pp. 452-461.
- Lee, S. et al. “Servo-Driven vs. Cam-Driven Forming: Efficiency and Defect Rate Analysis.” International Journal of Machine Tools and Manufacture, vol. 112, no. 4, 2021, pp. 78-85.
- Automotive Industry Action Group (AIAG). “Best Practices for Radiator Fin Manufacturing.” AIAG Supply Chain Guidelines, 2023.
- Patel, R. “Segmented Die Design for Reducing Friction in High-Speed Metal Forming.” Journal of Materials Processing Technology, vol. 298, no. 117, 2022, pp. 107234.
Suichang Lvye Machinery Co., Ltd.
We are one of the most professional radiator fin forming machine manufacturers in China, also support customized service with low price. We warmly welcome you to buy discount radiator fin forming machine for sale here from our factory. If you have any enquiry about quotation, please feel free to email us.
Address: No. 402, Mudanting East Road, Miaogao Street, Suichang County, Lishui City, Zhejiang Province
E-mail: L528753@outlook.com
WebSite: https://www.suichanglvye.com/
